Improve Industrial and Warehouse Management with Electronic Shelf Labels
In the world of massive supply chains and industrial storage we’re always dealing with paper labels and manual stock takes as a bottleneck. As item volumes and product counts go up, order volumes go up, the storage facilities are under pressure to meet the ever-increasing customer expectations. You need a smarter, more agile way of managing inventory.
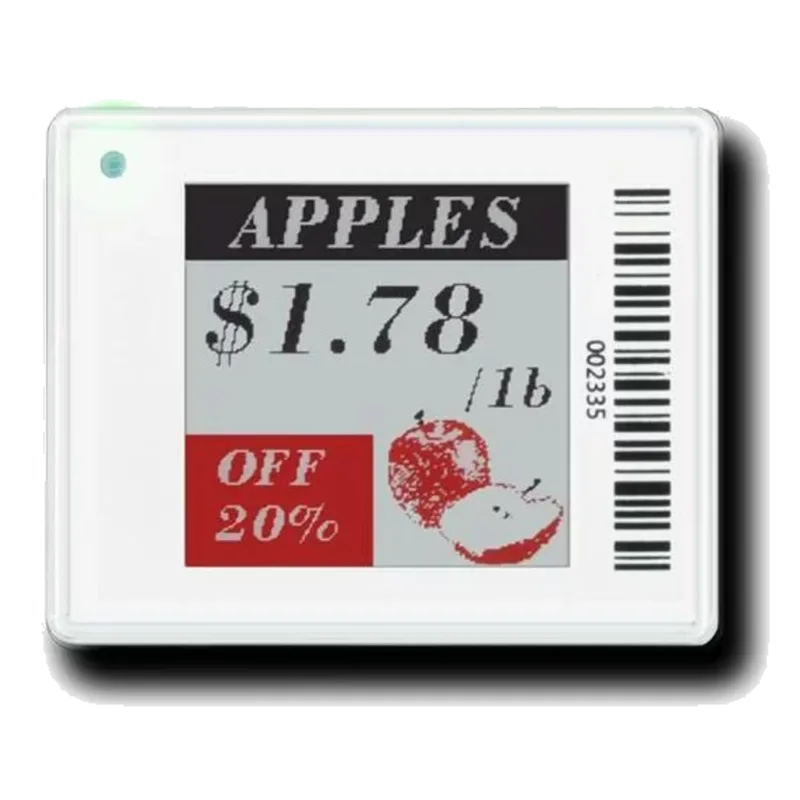
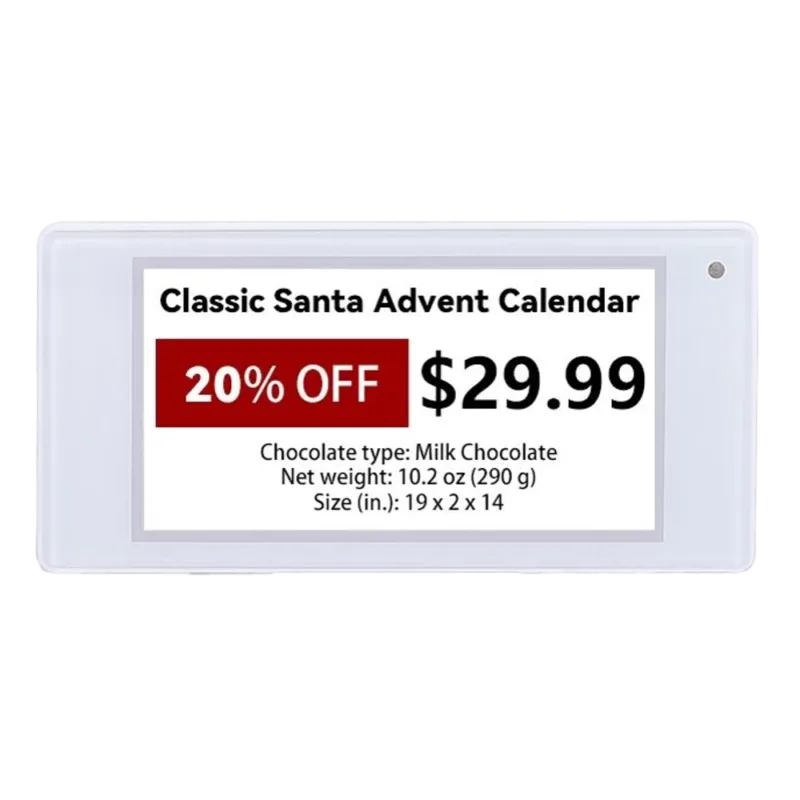
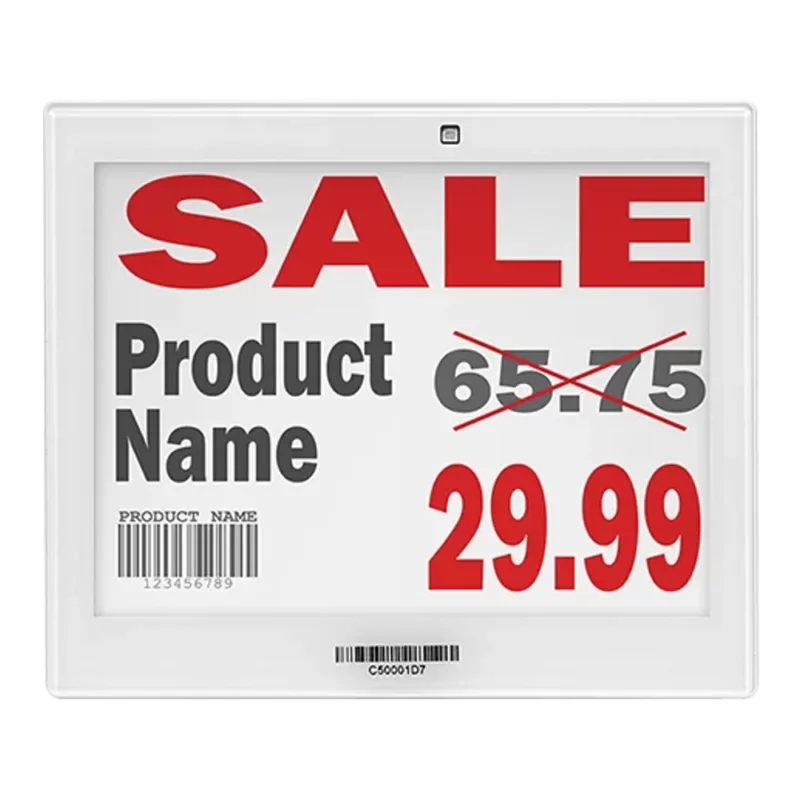
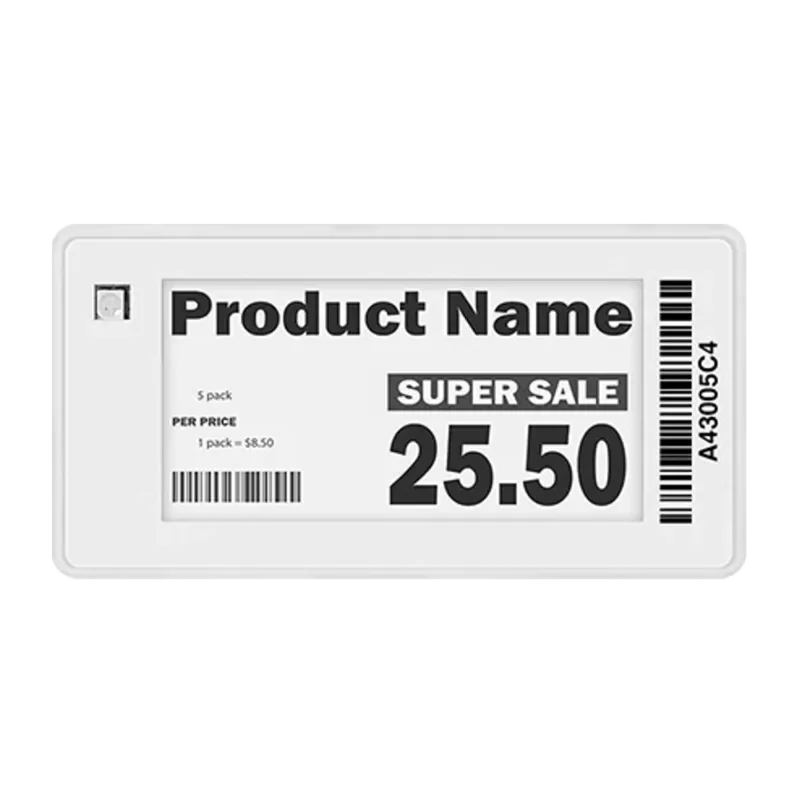
Enter Electronic Shelf Labels (ESL). They’re frequently linked with retail pricing but are also having a massive impact in the industrial, warehousing and materials management space. The use of smart tags and a cloud platform can be used to automate a whole range of processes and improve storage density. That’s a significant efficiency gain.
What are Industrial ESL Tags?
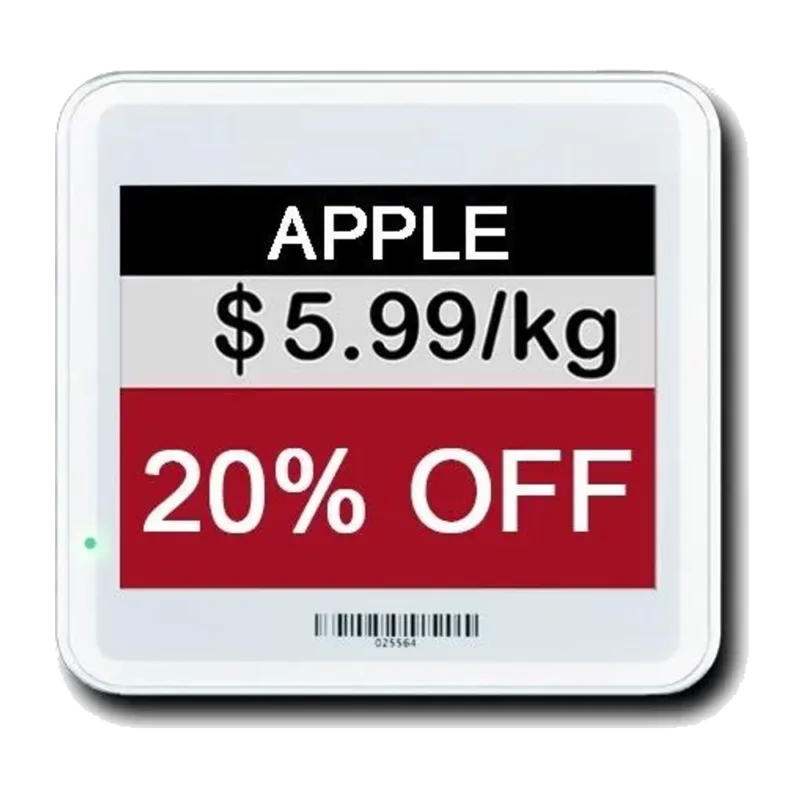
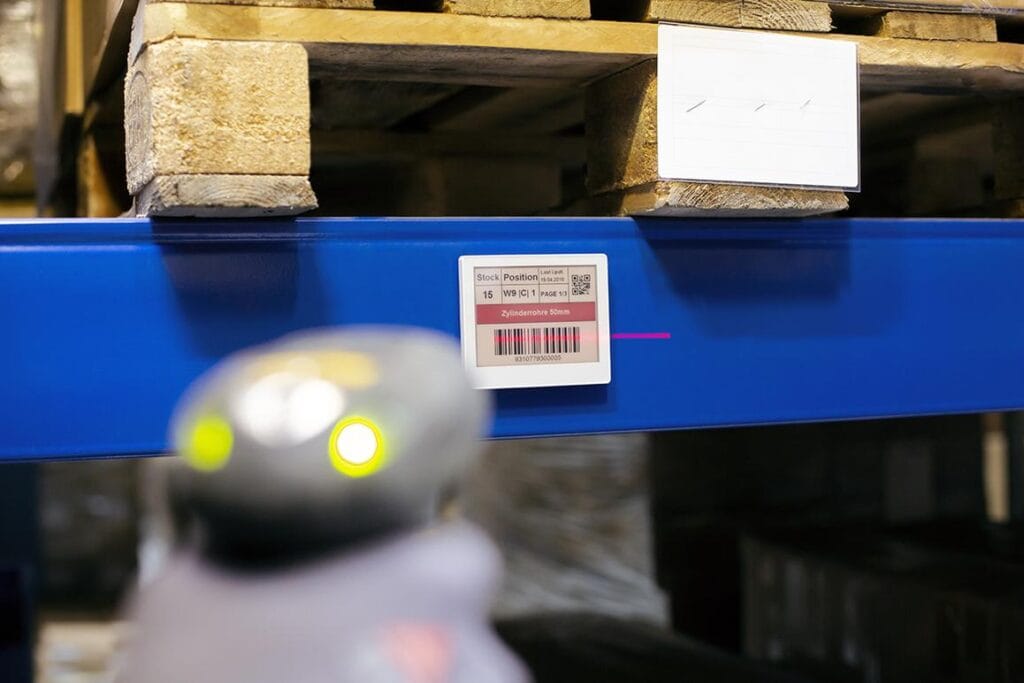
Electronic shelf labels are wireless, battery powered digital labels which are connected to a central cloud management system (CMS). They can be updated instantly and remotely via API and then display the dynamic information without requiring power and are visible in daylight and in direct light. There are even labels that are designed to work in sub-zero temperatures. They also have programmable LEDS which can flash different colours to indicate various information states.
Benefits of ESL in Warehouses and Industrial Plants
High Accuracy and Real-Time Synchronisation
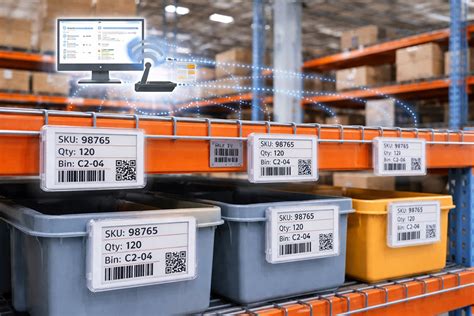
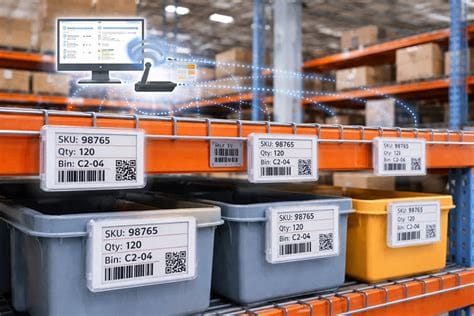
Electronic tags ensure that your inventory data, part numbers and stock levels are all in sync with your WMS (Warehouse Management System) and your ERP at all times. The labels can also be updated via handheld device at the shelf.
Streamlined Processes
Use ESL tags to highlight the exact location and quantity of an item during picking or put away. It saves the picker a huge amount of time searching for the item and will therefore speed up order cycle times considerably and reduce the potential for human error.
Unified Template Management
Industrial sites will often have thousands of different parts and components. The cloud platforms have a set of pre-defined unified display templates which will standardise the barcode, part description, QR code and stock level for the whole site.
Sustainability and Long-Term Durability
Built for the industrial environment, modern electronic labels have a very long life (often up to five years on a single replaceable battery). This leads to a massive reduction in paper consumption and removes the entire cost and hassle of manual label printing.
Beyond Warehousing: Versatile Industrial Applications
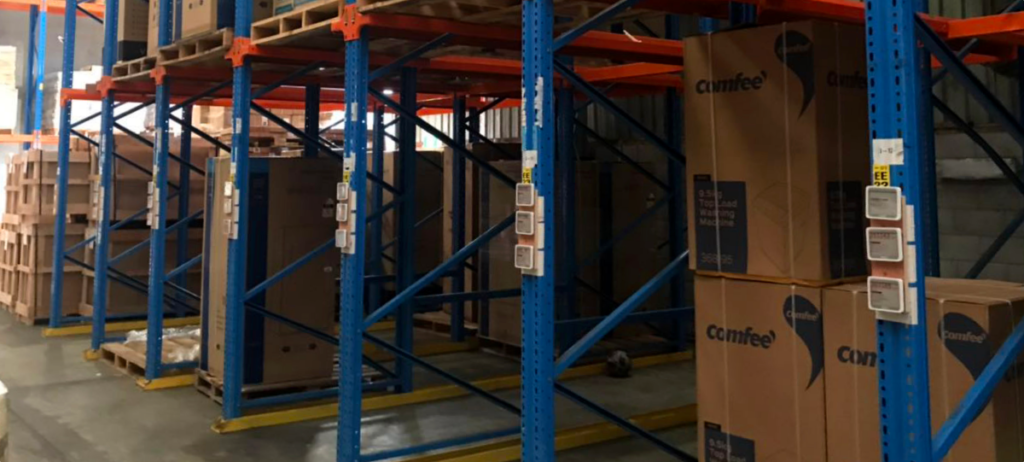
- Smart manufacturing and material chutes: ESLs can digitally label the material chutes, display digital buck sheets for internal movement and provide pick-by-light to confirm inventory levels at the point of pick.
- Healthcare & Inpatient Services: Hospitals use electronic tags to manage inpatient supply, track medical assets and control inventory.
- When warehouse layouts or storage zones are changing dynamically, the location codes and bin assignments can be updated remotely in seconds without any physical hardware being touched.
Future-Proof Your Operations with Digital Solutions
Moving away from paper tracking and into smart warehouse environments is no longer simply an upgrade, it’s a necessity if you want to be competitive. The move to electronic shelf labels in industry can deliver lower operating costs and help future proof your supply chain.
Ready to look at how our digital display and our ESL innovations can transform your site? Get in touch with us now to find out about our bespoke industrial solutions!